
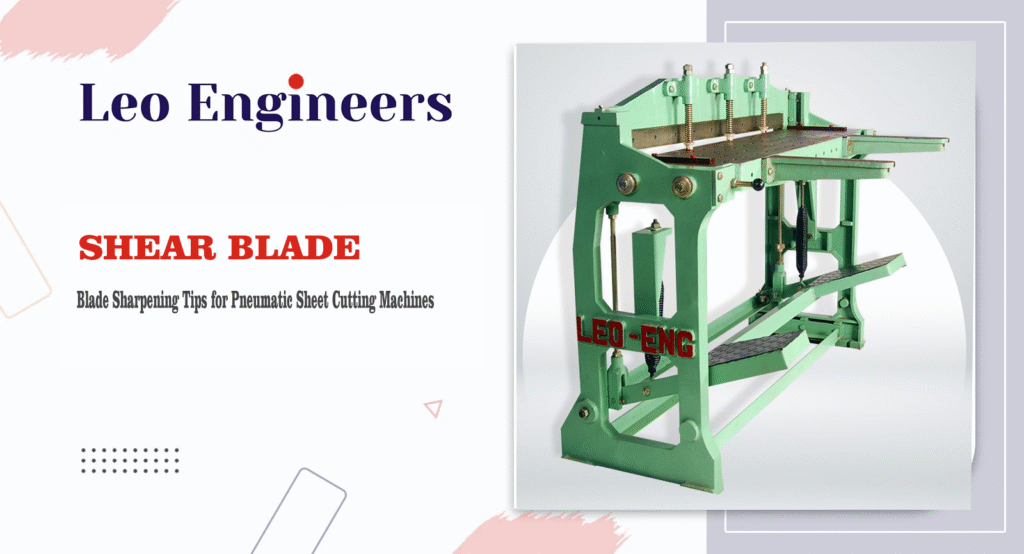
In any sheet metal workshop, the sharpness of your pneumatic shearing machine blade plays a pivotal role in the quality and consistency of your cuts. A dull shear blade doesn’t just slow down operations—it leads to rough edges, material distortion, excessive wear on your equipment, and compromised safety. Regular and correct sharpening is essential to maintain high precision and extend blade lifespan.
Why Blade Sharpening Should Be Routine
Pneumatic sheet cutting machines exert high force to shear metal sheets cleanly. Over time, even hardened steel shear blades dull due to constant friction, impact, and exposure to hard materials like stainless steel or galvanized sheets. Benefits of Regular Sharpening:- Smoother, burr-free cuts
- Reduced machine load and air pressure demands
- Less wear on pneumatic systems
- Fewer reworks and production halts
- Enhanced safety and control for operators
When Should You Sharpen the Blade?
Watch for these signs your shearing blade needs sharpening:- Edges of cut sheets are curling or have burrs
- Blade requires more pressure than usual to complete a cut
- Material shows signs of tearing, not shearing
- Operator effort increases even with foot pedal operation
- Irregular cut lines or frequent jamming
Pre-Sharpening Checklist
Before sharpening, ensure:- The blade is fully removed from the machine and properly labeled for top/bottom orientation.
- You’ve measured current blade angles (usually 23°–30° rake depending on material).
- You check for deep cracks or structural wear that may require a replacement instead of sharpening.
Step-by-Step Blade Sharpening Tips
1. Use a Precision Surface Grinder Avoid handheld tools or angle grinders—they remove material unevenly. Use a surface grinding machine with magnetic chucks for stability and uniform results. 2. Maintain the Correct Rake and Clearance Angle Don’t flatten the blade—follow the OEM-specified angle (usually between 23° to 30°). Deviating from this can cause improper clearance and faster wear. 3. Cool the Blade During Grinding Blade edges can overheat easily, resulting in hardening loss or micro-fractures. Always:- Use a water-based coolant system
- Grind in short passes with cooling intervals
- Avoid aggressive pressure
- Inspect the blade edge for consistency
- Remove burrs using a fine honing stone
- Test-fit to ensure edge alignment
How Often Should You Sharpen?
Recommended Schedule:- Mild Steel: Every 30–40 hours
- Stainless Steel or Hardened Alloys: Every 15–25 hours
- Light Gauge Aluminum or Copper: Every 50+ hours
Common Mistakes to Avoid
- Over-grinding and reducing blade height
- Sharpening at the wrong angle
- Ignoring hairline cracks before sharpening
- Not checking blade balance post-grinding
- Using damaged grinding wheels or dirty coolant




 Users Today : 12
 Users This Month : 197
 Total Users : 198
